How to Learn PLC Programming: A Competency-Gated Roadmap
Learn PLC programming through an evidence-led path from control fundamentals and scan execution to ladder logic, Structured Text, simulation, vendor tools, troubleshooting and a job-ready portfolio.
How to learn PLC programming in one answer
The most reliable way to learn PLC programming is to progress by evidence, not by elapsed weeks: understand the controlled process and electrical boundary; predict the PLC scan; write and trace basic ladder logic; manage time, events, state and abnormal conditions; use Structured Text and modular program structures where they fit; test in a disclosed simulator; reproduce the work in one target vendor environment; then diagnose hidden faults and document repeatable results.
A video watched, rung drawn or project downloaded is an activity. Competence means you can receive a requirement you have not memorized, predict the behavior before running it, implement it, test normal and abnormal cases, explain every state transition, identify a planted defect and leave evidence another person can review.
You do not need to buy an industrial controller on day one. Paper traces and a browser or desktop simulator can teach Boolean logic, scan behavior, timers, counters, sequencing and diagnostic reasoning. A vendor simulator or runtime adds target-specific project evidence. A guarded training bench adds wiring, modules and devices. Supervised field work adds real energy, process, access, cybersecurity and production constraints. These environments complement one another; none should impersonate the next.
What this roadmap owns
This page owns the broad learn PLC programming decision and practice roadmap. Adjacent pages retain their narrower tasks:
| Learner's next question | Specialist owner | Boundary |
|---|---|---|
| What is a PLC and how does it execute? | Beginner PLC programming pillar | concept lessons and language introductions |
| Which formal or online course should I buy? | PLC course comparison | provider and course selection |
| Which credential fits my experience? | PLC certification roadmap | issuer, eligibility, assessment and renewal evidence |
| How do I become a PLC technician? | PLC technician training roadmap | maintenance-role electrical, I/O, device and restoration competence |
| How do I become a programmer professionally? | PLC programmer career guide | job routes, applications, interviews and career progression |
| Which platform do I learn? | PLC software comparison | operating system, licence, target and simulation fit |
| What did a self-taught path get wrong? | Self-taught PLC lessons | experience-led mistakes and retrospective advice |
The older /blog/how-to-learn-plc-programming-2026-roadmap article covers the same task and should redirect here. Keeping two date-labelled versions would split links, create contradictory schedules and make search engines choose between near-duplicate owners.
Start by choosing the job-shaped outcome
“Learn PLC” can mean at least four different outcomes. Choose one primary destination for the first project cycle. You can widen later.
| Starting position | Existing advantage | First knowledge gap | Best first evidence |
|---|---|---|---|
| electrician or industrial electrical apprentice | circuits, drawings, devices and safe-work vocabulary | scan execution, state, software structure and test design | trace a motor request through input, logic, command and feedback |
| maintenance or production technician | process symptoms and machine familiarity | disciplined PLC monitoring, I/O mapping and change control | diagnose a hidden field-versus-logic disagreement without editing first |
| software developer | decomposition, data, testing and version control | physical I/O, cyclic execution, industrial risk and target constraints | implement one sequence in ladder and ST, then compare scan-by-scan state |
| engineering student or career changer | flexible learning time and fresh mental model | controls, electricity, software and industrial context together | complete a small simulated cell with drawings, code, tests and review notes |
| process or instrumentation practitioner | measurements, loops and process behavior | discrete sequences, controller program organization and digital diagnostics | scale an analog input, declare units/quality and test alarm/control boundaries |
Avoid choosing “master every PLC.” The IEC 61131-3:2025 Edition 4 public scope identifies Structured Text, Ladder Diagram and Function Block Diagram, with Sequential Function Chart elements for structuring organization. Vendors implement those ideas through different project models, tasks, libraries, instruction details and devices. Portable concepts matter; exact target evidence matters too.
Write a one-sentence outcome such as:
Within my authorized learning environment, I will be able to design, implement, test and explain a small discrete sequence; diagnose one hidden fault using an evidence path; and reproduce the result in the target tool used by the employers or equipment around me.
That statement is measurable. “Finish a PLC course” is not.
Gate 0: establish the safety and control-system boundary
PLC code can command hazardous motion, heat, pressure, electrical switching or chemical transfer. An HMI stop, software bit, interlock rung or simulator button is not an energy-isolation procedure. In the United States, OSHA 29 CFR 1910.147 addresses control of hazardous energy for covered servicing and maintenance; other countries and work have their own law, roles and procedures. Learn the applicable employer/site system before touching real equipment.
At this gate, you should be able to distinguish:
| Concept | Learner must be able to explain | Common dangerous shortcut |
|---|---|---|
| process command | what the PLC requests | assuming “off” makes equipment safe to work on |
| final control element | relay, contactor, drive, valve or other device that acts | treating an output bit as proof of physical state |
| feedback | independent evidence of field condition | using the command as its own feedback |
| protective/safety function | separately engineered risk-reduction function where required | inventing a universal emergency-stop rung in standard logic |
| isolation and verification | site- and task-specific energy control by authorized people | relying on software, a screen or a stopped sequence |
| change authority | who may connect, upload, force, edit, download and return to service | practicing an online edit on production because it worked in simulation |
Also learn the information path: sensor condition → input electronics → controller tag/image → executed logic → output command → output electronics → final element → process → independent feedback. This path becomes the backbone for programming and troubleshooting.
Gate 0 assessment: given a simple conveyor drawing and symptom, label the command, feedback, standard control, protective boundary and evidence you would need before any physical test. If you cannot state what is simulated and what requires authorized field work, remain at this gate.
Gate 1: build the PLC execution mental model
The beginner mistake is to read ladder as a static electrical drawing. PLC behavior depends on execution: input acquisition, scheduled program/task execution, state retained by instructions or variables, communications/housekeeping and output updates. Exact ordering and timing depend on the configured controller, task and I/O architecture; “read every input, solve everything, write every output” is a useful introductory model, not a universal timing specification.
Learn these six ideas before collecting instructions:
- Boolean state: a contact instruction evaluates data; it is not the physical contact itself.
- execution order: logic evaluated earlier can affect logic evaluated later in the same execution, subject to program structure and platform semantics.
- previous state: edge, timer, counter, latch and sequence behavior depends on stored history.
- task timing: periodic, continuous/event tasks, communications and I/O updates can create different data ages.
- startup and restart: initial, retained, warm-start and fault-recovery behavior must be designed and tested for the exact target.
- observation effects: online status is sampled and presented by software; a green rung is not a perfect oscilloscope or proof of the field circuit.
Run a six-scan paper trace
Use a start request, stop permit and running memory. Declare the learning semantics first:
RunRequest := StopPermit AND (StartPB OR RunRequest_previous)
MotorCommand := RunRequest AND NOT Fault
| Scan | StopPermit | StartPB | Fault | Previous RunRequest | New RunRequest | MotorCommand |
|---|---|---|---|---|---|---|
| 1 | 1 | 0 | 0 | 0 | 0 | 0 |
| 2 | 1 | 1 | 0 | 0 | 1 | 1 |
| 3 | 1 | 0 | 0 | 1 | 1 | 1 |
| 4 | 1 | 0 | 1 | 1 | 1 | 0 |
| 5 | 0 | 0 | 0 | 1 | 0 | 0 |
| 6 | 1 | 0 | 0 | 0 | 0 | 0 |
This is a learning example, not a complete motor-control or safety design. It deliberately separates remembered request from output command so a fault can remove the command. A real design must define restart, overload, drive, feedback, mode, permissive, protective and recovery behavior.
Gate 1 assessment: predict every cell before running the example. Then change the program order or initialization assumption and explain the changed result. You pass when your trace and execution agree for stated semantics, including restart.
Gate 2: learn ladder logic as executable Boolean and state logic
Start with a small instruction vocabulary and many tests. Contacts, coils, branches and comparisons teach Boolean reasoning. Timers, counters, edges and set/reset constructs introduce state. Avoid memorizing pictures without declaring truth behavior.
Build in this order:
| Exercise | Required concepts | Abnormal test | Evidence to keep |
|---|---|---|---|
| Boolean permissive | series, parallel, negation and named intermediate state | conflicting start and inhibit | complete truth table and scan trace |
| maintained request | seal-in or explicit state with reset priority | start and stop arrive together | declared priority and restart table |
| timed state | on-delay behavior and reset | input drops just before done | input/event timeline and timer fields |
| item count | rising edge plus count and reset | signal remains high or chatters | event list proving one count per accepted event |
| two-step sequence | state, transition and outputs by state | transition sensor never arrives | timeout/fault result and recovery rule |
| mode arbitration | manual/automatic command ownership | both requests active | priority matrix and denied-command reason |
Do not teach emergency-stop behavior as an ordinary “NC contact in a rung.” A ladder symbol can model a condition for learning, but a required safety function needs risk assessment, appropriate architecture, devices, validation and applicable standards. Keep standard sequence practice and functional-safety competence explicitly separated.
Gate 2 assessment: receive a new two-actuator requirement; write an I/O list, Boolean conditions, transition table and abnormal cases; implement it without copying an earlier solution; and explain the result scan by scan.
Gate 3: add timers, counters, edges, analog values and state machines
Many programs fail not because the Boolean expression is wrong but because time and state were undefined. Ask what happens on enable, interruption, retrigger, reset, startup, overflow and conditional execution. Then check the exact instruction documentation for the chosen target.
| Requirement question | Likely construct | Tests that expose weak understanding |
|---|---|---|
| has a condition stayed valid long enough? | on-delay timing | bounce, dropout before done, task-time change |
| should an output persist after an input changes? | off-delay or explicit timed state | retrigger and restart |
| did an event occur once? | rising/falling edge | input already true at startup, conditional invocation |
| how many accepted events occurred? | edge plus counter | held input, burst input, reset while active |
| which phase owns the outputs? | state machine or SFC structure | impossible transition, timeout, recovery and manual mode |
| how does a measurement become engineering units? | raw input, scaling, quality/range and alarm logic | under-range, over-range, bad quality and unit mismatch |
For a sequence, separate state, transition, command and fault. A compact filling example might have Idle, Fill, Settle and Complete states. FillValveCommand is true because the sequence is in Fill and all command permits are valid. The level-high feedback is a transition condition, not proof that the commanded valve moved. A fill timeout is a diagnostic result; it should not silently jump to Complete.
Download the PLC learning project acceptance matrix and require at least normal, boundary, conflicting-command, missing-feedback, timeout, reset and restart cases for every stateful project.
Gate 3 assessment: implement a four-state batch or conveyor sequence, inject a missing transition, and produce a trace that identifies current state, command, expected feedback, elapsed time and first failed condition.
Gate 4: learn Structured Text and modular design without abandoning ladder
Structured Text is useful for calculations, data transformation, arrays, loops, reusable algorithms and explicit state machines. Ladder remains strong where maintenance teams need fast Boolean/status visibility. Function Block Diagram often suits signal flow and control blocks. The correct choice depends on the problem, target support, team, lifecycle and testability—not a claim that one language is universally modern or superior.
Translate one already-tested ladder exercise into Structured Text. Preserve the same I/O contract and test matrix:
IF Reset OR NOT StopPermit THEN
    RunRequest := FALSE;
ELSIF StartPB THEN
    RunRequest := TRUE;
END_IF;

MotorCommand := RunRequest AND NOT Fault;
This generic teaching fragment does not declare a vendor, safety behavior or complete restart policy. Its value is comparison: the same state and priority should produce the same expected cases in both representations.
Then learn program organization:
- separate physical I/O mapping from sequence logic;
- name data by meaning rather than raw address alone;
- keep commands and feedback distinct;
- define function/function-block inputs, outputs, state and error behavior;
- keep mode ownership explicit;
- centralize state transitions instead of scattering step writes;
- record assumptions, units, ranges and revision;
- design diagnostic state at the same time as control state.
Gate 4 assessment: implement the same stateful requirement in two supported languages, run an identical event matrix, explain any target-specific semantic difference and justify which representation the intended maintainer should receive.
Gate 5: use simulation as a deliberate practice loop
Simulation is most valuable when it makes a prediction falsifiable. The loop is:
- write the requirement and expected result;
- choose known initial state;
- apply a recorded input event;
- observe logic and state;
- compare actual with expected;
- explain the first disagreement;
- change one justified thing;
- rerun the full matrix;
- save the revision and evidence.
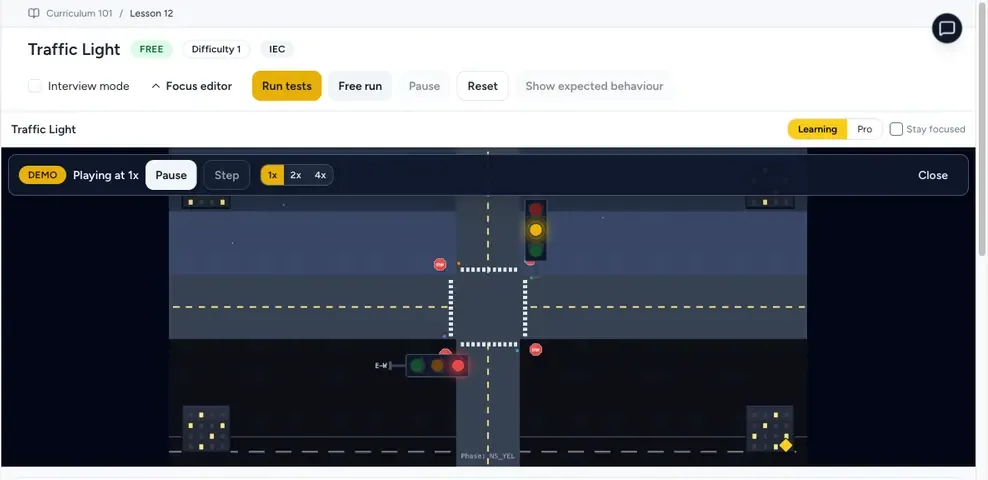
Match the tool to the claim:
| Environment | Good learning evidence | What it cannot establish alone |
|---|---|---|
| paper/table trace | Boolean, priority and declared scan reasoning | executable syntax or target behavior |
| browser learning simulator | repeatable learning-dialect logic, state and fault practice | exact vendor compile, controller firmware, physical I/O or machine validation |
| CODESYS/OpenPLC or another desktop runtime | supported language/runtime behavior for recorded versions and configuration | unrelated vendor targets or physical installation |
| vendor offline simulator/emulator | exact project compile and supported simulated controller behavior | excluded modules, electrical response, plant process or final-element behavior |
| guarded low-energy bench | wiring, channels, devices, downloads and measured response | production hazards, site network and full machine acceptance |
| supervised field work | actual asset, process, access and handover evidence | competence beyond the observed system and authorization |
Practice a graded PLC sequence in the browser when you need repeatable logic and troubleshooting cases. Treat the result as evidence for the disclosed learning environment only. It does not validate a TIA Portal, Studio 5000, CODESYS, TwinCAT, Sysmac Studio, GX Works or EcoStruxure project; a real controller; field wiring; a machine; a process; or a safety function.
Gate 5 assessment: complete one unseen scenario, submit the predicted matrix before execution, diagnose a planted defect and reproduce the corrected result from a reset state.
Gate 6: specialize in one target ecosystem
Choose a first vendor by local evidence: installed equipment, job descriptions, employer access, instructor/lab access and operating-system/licensing feasibility. Do not choose from global market-share folklore. Exact software editions, licences, simulator availability, controller compatibility and training offers change; verify them on current vendor pages before paying.
| Selection evidence | Question to answer | Record in your decision |
|---|---|---|
| local installed base | which controller families appear on equipment you may legally train for? | family, generation and source/date |
| target roles | which platforms recur in a sample of relevant vacancies? | region, job level, sample window and count |
| tool access | can you legally obtain the engineering tool and needed features? | edition, version, OS, licence/trial limits |
| simulation | what CPU, instructions, communications or devices are supported? | exact exclusions and evidence link |
| hardware access | is there a guarded bench, school lab or employer training rack? | CPU/module/firmware and supervision |
| learning support | are official manuals, examples and structured training available? | document/course identifiers and dates |
Rebuild one completed generic project in the chosen tool. Capture the exact software version, project type, controller target, configured task/program order, tags, compile result, simulator/controller used and test result. Learn upload/download terminology, online monitoring, cross-reference, diagnostics, backup/restore and change-control basics for that environment.
Official starting points include Siemens SCE learning/training documents, Rockwell Automation training services, CODESYS first steps, Beckhoff TwinCAT 3 PLC documentation, Schneider Electric product documentation, Mitsubishi Electric FA manuals and Omron industrial automation manuals. A vendor page is evidence of its own offering, not proof that the tool fits your employer or region.
Gate 6 assessment: a reviewer can open the recorded target project, reproduce the declared tests and understand what was simulated, what ran on hardware and what remains unverified.
Gate 7: add I/O, analog, networking and process evidence
Programming becomes industrial automation when logic meets data and devices. Expand gradually:
| Layer | First practical task | Required evidence |
|---|---|---|
| discrete I/O | map a sensor and command with independent feedback | electrical drawing, address/tag map, observed channel and state trace |
| analog I/O | scale raw input into named engineering units | raw range, engineering range, equation, clamp/quality and injected boundary values |
| HMI | expose status, command eligibility and diagnostic reason | tag contract, mode/authority, invalid-command response and alarm test |
| drive/device | exchange command, status and fault information | exact device/manual, connection/map, state words and loss/recovery behavior |
| industrial network | identify controller, device, path and cyclic/explicit data role | topology, addresses/identity, diagnostics, mapping and authorized change record |
| process control | close a simulated or guarded loop | units, direction, limits, sample/task timing, disturbances and acceptance criteria |
For cybersecurity, do not create a casual home-lab habit of bridging engineering tools into live operational networks. NIST SP 800-82 Rev. 3 treats OT security in the context of performance, reliability and safety. Access, accounts, removable media, remote connections, software sources, backups and changes belong inside the organization’s authorized controls.
Gate 7 assessment: trace one value from a known field or simulated condition through acquisition, controller data, logic, command and feedback, then identify the first boundary that disagrees during a hidden fault.
Gate 8: learn troubleshooting before calling yourself job-ready
Random edits are not troubleshooting. Begin with the symptom, expected behavior, safe/authorized boundary and known change history. Then split the evidence chain and find the first disagreement.
Use this worksheet sequence:
| Step | Question | Evidence |
|---|---|---|
| 1 | What exactly is the symptom and asset? | time, mode, state, operator report and reproducibility |
| 2 | What should happen under the approved requirement? | drawing, narrative, sequence or known-good record |
| 3 | What changed? | maintenance, recipe, version, device, network or environment history |
| 4 | Is the PLC healthy and executing the expected project? | controller/task/program status, identity and version |
| 5 | Does the physical/simulated condition reach the input data? | measured/known condition, module/channel and tag |
| 6 | What is the first false permissive or failed transition? | online trace or recorded state, without changing logic |
| 7 | Is the output command present? | command owner, inhibit/fault/mode reason and output tag |
| 8 | Does the command reach the final element? | output/device state and authorized measurement |
| 9 | Does the process response return as feedback? | independent feedback and expected time window |
| 10 | Does the smallest justified correction survive regression? | repeated normal, abnormal, restart and handover tests |
Download the PLC learning fault-isolation worksheet. It prevents a learner from jumping from symptom to code change without recording the boundary test.
Gate 8 assessment: diagnose two unseen defects—one in logic/state and one outside it—without being told the category. Score the hypothesis quality, test order, unsafe action avoidance, correction, regression and handover, not merely time to green.
A flexible 12-week practice cycle
Calendar duration depends on prior knowledge, hours, feedback, tool access and target complexity. Use this as one approximately 8–10-hours-per-week cycle, not a guarantee of employment or field authorization.
| Weeks | Focus | Deliverable | Exit evidence |
|---|---|---|---|
| 1–2 | control boundary, I/O path and scan model | annotated system diagram and paper traces | explain state, timing and physical-versus-logical boundary |
| 3–4 | Boolean ladder, modes and maintained state | motor/request and permissive exercises | truth/priority/restart matrix passes |
| 5–6 | timers, counters, edges and sequence | conveyor or batch sequence | normal, timeout, conflict and reset cases pass |
| 7 | Structured Text and program organization | equivalent ST/state implementation | same behavior contract passes in two representations |
| 8 | deliberate simulator testing | unseen scenario and planted fault | prediction, trace, diagnosis and regression evidence |
| 9–10 | one vendor ecosystem | compiled target project | versioned project and supported simulation/target evidence |
| 11 | I/O/analog/device or guarded bench | one end-to-end value path | map, units, diagnostics and boundary trace |
| 12 | hidden-fault assessment and portfolio | evidence pack and review | reviewer can reproduce claims and identify exclusions |
Repeat the cycle at higher complexity: more states, analog quality, reusable blocks, HMI/device integration, networks and role-specific work. Do not rush into motion, robotics, high-energy panels or safety application programming without the appropriate formal learning, hardware, supervision, authorization and validation context.
Build five portfolio projects with acceptance criteria
A useful portfolio is not a screenshot gallery. Each project should include the requirement, environment, I/O/data contract, state or sequence design, source, tests, defects found, result, limitations and revision.
| Project | Design depth | Minimum abnormal evidence |
|---|---|---|
| start/stop command with feedback | request, permit, command, feedback and restart policy | start/stop conflict, fault, feedback timeout and restart |
| indexed conveyor or sorter | event edge, count/position state and actuator timing | stuck sensor, missed feedback, timeout and reset |
| tank/batch sequence | explicit states, transitions, commands and alarms | impossible initial state, fill timeout, manual/auto conflict |
| analog measurement/control | scaling, units, quality/range and trend | under/over-range, bad value and saturation/limit behavior |
| networked device or simulated peer | identity, connection/data map and diagnostic status | connection loss, stale/bad data and controlled recovery |
Use the PLC learner evidence-pack checklist. Remove credentials, proprietary code, plant identifiers, IP addresses and confidential drawings. Never publish an employer project to prove you worked on it.
Practical assessment rubric
| Dimension | 0: absent/unsafe | 1: partial | 2: repeatable evidence |
|---|---|---|---|
| requirement | copies a pattern without behavior contract | normal behavior stated | normal, abnormal, restart and exclusions declared |
| design | outputs written from scattered conditions | readable logic | state/ownership/diagnostics explicit and reviewed |
| prediction | runs until something works | predicts normal case | predicts all recorded cases before execution |
| implementation | unexplained warnings or hidden state | compiles/runs | versioned, named, documented and reproducible |
| testing | one happy-path demonstration | several manual checks | resettable matrix with expected/actual evidence |
| troubleshooting | random edit/force | finds defect after prompting | first-disagreement method on an unseen fault |
| safety/boundary | claims simulation proves machine safety | basic disclaimer | exact environment, authorization and unverified layers stated |
| handover | screenshot only | short description | requirement, source, version, tests, result and next risk included |
A project scoring 16/16 is not universal professional certification. It is strong evidence for the declared task and environment.
How to choose courses, certificates and hardware
Courses help when they supply sequence, feedback, labs or equipment you cannot obtain alone. Judge the evidence, not video hours.
| Purchase | Buy when | Verify before payment | Delay when |
|---|---|---|---|
| online course | it closes a named knowledge gap and includes relevant practice | syllabus, instructor, tool/version, labs, feedback, access and refund terms | free official material plus practice already covers the task |
| vendor training | target ecosystem is supported by job/equipment evidence | region, prerequisites, software/hardware, assessment and current dates | no target platform chosen |
| certificate/certification | issuer and employer recognize the exact credential | eligibility, assessment, renewal, fees and credential type | it is being used as a substitute for practical evidence |
| simulator licence | required scenarios, state visibility or export justify it | instruction semantics, limits, persistence and product facts | a free environment proves the current learning objective |
| PLC/training bench | physical I/O competence is the next gate | voltage, isolation, modules, software/licence and supervision | ladder/scan/state basics are not yet repeatable |
ISA distinguishes professional certifications and certificate programs; review the exact ISA certification directory and eligibility pages. Rockwell and Siemens publish platform-specific workforce training and regional offerings. These are options, not a universal prerequisite. The best first credential for an experienced technician may be wrong for a beginner programmer.
Common learning failures and their correction
| Failure pattern | Why it stalls | Better practice |
|---|---|---|
| watching without predicting | recognition feels like competence | pause, declare expected state, then execute |
| collecting instructions | syntax grows while design remains weak | use a small vocabulary across many unseen cases |
| buying hardware first | setup cost hides the logic gap | prove scan/state/testing in software, then add a bench |
| learning three vendors at once | tool navigation consumes practice time | choose one target after portable fundamentals |
| copying a seal-in rung | hidden priority/restart assumptions remain | build a truth, priority and restart matrix |
| calling output status “machine running” | command and feedback are conflated | model independent feedback and timeout |
| treating simulation as commissioning | physical and target-specific layers are missing | label the evidence environment and handoff tests |
| editing before isolating | the symptom moves and evidence is destroyed | record first disagreement before changing anything |
| publishing employer code | creates confidentiality and security risk | build sanitized original projects and diagrams |
| choosing by salary claims | occupation, region and experience are blurred | sample relevant local roles and official occupation data |
For a first end-to-end portfolio exercise, follow the home PLC two-tank training project. It connects an I/O list, state machine, runnable Structured Text, modeled plant, injected faults and acceptance evidence without requiring live mains-powered equipment.
Frequently asked questions
What is the best way to learn PLC programming?
Use a competency-gated loop: learn the control and scan model, predict a small behavior, implement it, test normal and abnormal cases, diagnose a hidden defect and keep evidence. Add one vendor tool and physical practice only when the previous layer is repeatable.
Can I learn PLC programming by myself?
Yes, many fundamentals can be self-directed: Boolean logic, scan reasoning, ladder, Structured Text, sequencing, simulation and documented testing. Seek qualified instruction and supervision for real electrical work, machinery, safety functions, high-energy systems and employer-specific authorization.
How long does it take to learn PLC programming?
There is no defensible universal duration. Prior electrical/programming knowledge, weekly practice, feedback, target platform and the definition of “learned” change the answer. Use the gate assessments on this page; count repeatable capabilities rather than months.
Do I need a degree to program PLCs?
Requirements vary by role, employer, country and regulated scope. Some enter through engineering degrees, technical colleges, apprenticeships, maintenance/electrical work or structured self-study. Review actual local vacancies and authorization requirements rather than assuming one route fits every job.
Which PLC should a beginner learn first?
Begin with portable execution and logic concepts, then choose one ecosystem supported by local equipment, relevant jobs, legitimate software access and lab support. Do not infer a platform from unverified global market-share claims.
Should I learn ladder logic or Structured Text first?
Ladder is often a clear first representation for Boolean control and maintenance-visible conditions. Add Structured Text for calculations, data and explicit algorithms. Eventually compare both against the same test contract and use the representation that fits the target, team and task.
Can I learn PLC programming without hardware?
You can learn substantial logic, scan, state, testing and troubleshooting skills without hardware. You cannot claim physical I/O, wiring, device, timing, machinery or safety validation from software alone. Add a guarded bench and supervised field experience when those are the next objectives.
Is free PLC software enough to learn?
It can be enough for early gates if it supports the required language, execution visibility, reset, tests and persistence. Record the exact version, runtime/target and limitations. Free access does not make one environment equivalent to every commercial controller.
What projects should a beginner build?
Build a permissive/start-stop example, timed sequence, counted conveyor/sorter, four-state batch, analog scaling/control task and a network/device diagnostic case. Require abnormal, timeout, reset and restart tests, not only a successful animation.
How do I know when I am ready to apply for PLC jobs?
Apply when you can solve an unseen small requirement, explain scan/state behavior, use one relevant target tool, diagnose hidden faults systematically and present sanitized evidence. Job readiness still depends on the specific role’s education, electrical, travel, process and experience requirements.
Are PLC certifications required?
Not universally. A credential can support a specific role when its issuer, eligibility and assessment match employer needs. It does not replace target-project evidence, safe-work qualification or supervised experience. Verify the exact current credential before paying.
How should a software developer approach PLC learning?
Spend less time on basic syntax and more on cyclic execution, task/I/O timing, retained state, physical feedback, failure modes, industrial networking, access control and controlled change. Do not import web-development deployment habits into operational technology without understanding consequence and authorization.
How should an electrician approach PLC learning?
Use existing circuit/device strength, then focus on data truth, scan order, state machines, software organization, target diagnostics and test evidence. Keep the physical circuit, input state, logic condition, output command and actual feedback distinct.
Does a PLC simulator prove my program will work on a real machine?
No. It can prove the declared behavior in the disclosed simulated environment. Target compilation, supported instruction semantics, I/O electronics, device integration, timing, process response, risk controls and machine acceptance need additional evidence in the appropriate environment.
Sources and verification trail
Transactional details, courses, software versions, credentials and regional offerings change. Verify them on the linked first-party page at the time of use.
- IEC 61131-3:2025 Edition 4—Programming languages
- PLCopen: IEC 61131-3 programming languages overview
- OSHA 29 CFR 1910.147—Control of hazardous energy
- OSHA control-of-hazardous-energy overview
- NIST SP 800-82 Rev. 3—Guide to Operational Technology Security
- CODESYS Development System—First steps
- CODESYS online monitoring and breakpoint documentation
- OpenPLC project documentation
- Siemens SCE learning and training documents
- Siemens SITRAIN training catalog
- Rockwell Automation workforce development and training
- Rockwell Automation certificate programs
- Beckhoff TwinCAT 3 PLC introduction
- Schneider Electric product documentation portal
- Mitsubishi Electric Factory Automation downloads
- Omron Industrial Automation support and manuals
- ISA certification directory
- ISA CCST Body of Knowledge
- US Department of Labor: advanced-manufacturing apprenticeships
- US BLS: Industrial machinery mechanics, maintenance workers and millwrights
- US BLS: Electrical and electronics engineers
Continue with the right specialist
- Learn concepts in the beginner PLC programming pillar.
- Practice the ladder logic tutorial and Structured Text guide.
- Choose software with the PLC programming software comparison.
- Build projects from the practical PLC programming exercises.
- Learn systematic diagnosis in the PLC troubleshooting guide.
- Compare credentials in the PLC certification roadmap.


